
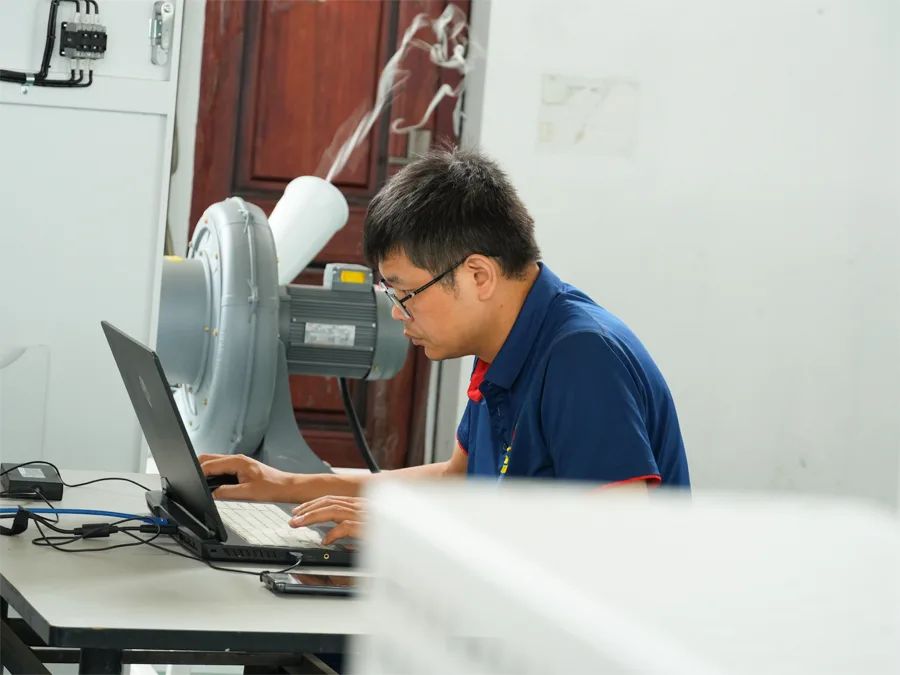
Ouyang Ning
PLC Programmer, JOTA MACHINERY
Ouyang Ning is the programmer behind Jota’s machines, giving them the logic that drives every motion. Specializing in PLC and HMI programming, he designs control systems that ensure smooth operation, safety, and efficiency from the moment a machine is powered on. His work transforms complex hardware into intelligent systems operators can run with confidence.
Known for his precision coding and problem-solving mindset, Ouyang develops clear, reliable programs that are both technically strong and user-friendly. He believes programming is more than code—it’s a responsibility. Each logic sequence, each HMI screen, and each safety interlock reflects his philosophy: machines must earn trust through stable performance.
For Ouyang, it’s about discipline, clarity, and continuous improvement. From writing ladder logic to debugging on the factory floor, he ensures Jota’s machines deliver flawless production—where invisible code creates visible results.
The Human Side of Logic: Ouyang Ning’s Role at Jota Machinery
In the world of industrial machinery—where precision depends on signals, logic, and control—Ouyang Ning brings something more: clarity and reliability.
As PLC Programmer at Jota Machinery, Ouyang designs the invisible logic that powers every machine. From ladder logic to HMI design, he transforms mechanical complexity into programs that operators can use with ease. His coding ensures that slitter rewinders start safely, run smoothly, and deliver consistent results under real production conditions.
For Ouyang, programming is never just about writing code—it is about responsibility. Every alarm message, every logic sequence, every safety interlock reflects his belief that machines must not only perform, but also protect operators and build customer confidence.
To him, the greatest satisfaction comes when a machine runs at full speed without alarms, and the client smiles with relief. In his philosophy, invisible code creates visible trust.
The Brain of the Machinery: PLC
At Jota Machinery, PLC programming is the hidden force that keeps every system precise and dependable. Our programmers design the control logic that connects motors, sensors, and operator commands into one seamless process. From ladder logic to HMI interfaces, every line of code is written to ensure safety, stability, and efficiency on the production floor.
This work is not just about automation—it’s about responsibility. The logic behind each machine must protect operators, adapt to different materials, and perform reliably under pressure. That is why we call the PLC the brain of the machinery: it gives every unit intelligence, discipline, and consistency from the first startup to long-term operation.
Every machine at Jota Machinery has a hidden heartbeat—the logic that makes motors run, sensors respond, and processes flow smoothly. Behind this invisible intelligence is Ouyang Ning, our dedicated PLC Programmer. His role is to turn engineering requirements into precise control code, ensuring that each slitter rewinder and converting line operates with safety, speed, and reliability.
Turning Code Into Motion
Ouyang’s work begins long before a machine leaves the factory. He writes and tests ladder logic, structured text, and HMI programs that define how the machine behaves. From unwinding to slitting to rewinding, every motion depends on his programming. His precision ensures operators can run complex systems with confidence, even if they are new to automation.
A Methodical Approach to Debugging
When debugging, Ouyang follows a systematic process: check the hardware and wiring, verify I/O signals, trace the logic flow step by step, simulate functions when possible, and finally, run incremental tests until stability is achieved. This structured method saves valuable time and prevents small errors from becoming major delays during commissioning.
Making Programs Operator-Friendly
For Ouyang, PLC programming is not just about writing code—it’s about designing a system that works for people. He develops clear HMI interfaces with intuitive layouts and plain-language alarm messages. Instead of showing “Error 203,” his screens display actionable messages like “Check left photoelectric sensor,” allowing operators to respond quickly without needing an engineer at their side.
Balancing Standardization and Flexibility
One of his guiding principles is balance. Core modules—such as motor start/stop, alarm handling, and safety interlocks—are standardized for reliability. But every customer has unique raw materials, production speeds, and operator habits. Ouyang builds flexibility into his programs, allowing adjustments to parameters like tension, speed, and cut length without rewriting the code.
Challenges That Shape Expertise
Some of his toughest problems have become his proudest achievements. In one case, a rewinder’s tension fluctuated at high speed, and many assumed it was a mechanical fault. After investigation, Ouyang discovered the issue was in the PID loop sampling time inside the PLC. By adjusting the loop timing and filtering the sensor input, he stabilized the tension—a reminder that sometimes software is the solution to mechanical challenges.
Staying Ahead of Technology
In a fast-moving industry, Ouyang constantly updates his knowledge. He follows Siemens and Mitsubishi advancements, attends automation expos, and studies Industry 4.0 applications like IoT integration and predictive maintenance. By staying current, he ensures that Jota Machinery’s automation systems remain competitive and aligned with global trends.
Philosophy and Responsibility
Ouyang believes programming is a responsibility as much as a technical skill. “Every line of code must serve reliability,” he says. His focus is on making sure machines are safe, efficient, and easy for operators to use. To him, invisible logic has a very visible impact: it shapes customer trust and production success.
The Most Rewarding Moment
What gives him the most satisfaction? It’s the moment a newly delivered machine runs at full speed, without alarms, and the client smiles with relief. “It feels like I’ve given the machine a heartbeat,” Ouyang says. For him, that is the ultimate reward—seeing his logic become real-world productivity.
Closing Thoughts
Ouyang Ning embodies the unseen strength of Jota Machinery. His work may be hidden in the code, but its results are clear in every smooth cut, every stable roll, and every satisfied operator. Through precision, discipline, and dedication, he turns complexity into clarity, and logic into trust.
Q&A with Ouyang Ning – PLC Programmer
Invisible code, visible performance.
I’ve always enjoyed problem-solving, especially when it comes to connecting hardware with logic. PLC programming is where mechanical motion, electrical signals, and digital logic meet. The idea that a few lines of code can bring an entire machine to life fascinated me early in my career.
At Jota, we mainly use Siemens and Mitsubishi PLCs, but I’ve also worked with Omron and Allen-Bradley depending on customer requests. Each brand has its own strengths. Siemens is very versatile for structured automation, Mitsubishi is compact and cost-efficient, while Allen-Bradley integrates well with large-scale SCADA systems.
My process is always structured: Check power and wiring – make sure the hardware is correct. Look at I/O signals – verify sensors and actuators are responding. Trace logic flow – follow the ladder logic or structured text step by step. Run simulation if possible – isolate the problem virtually. Test incrementally – fix one issue at a time. This systematic approach prevents wasted time chasing symptoms instead of root causes.
Once, during a machine installation abroad, the rewinder tension kept fluctuating at high speed. The issue turned out to be not hardware but sampling time in the PID loop inside the PLC. After adjusting the loop timing and filtering the sensor input, the tension stabilized. It reminded me how software can solve what looks like a mechanical fault.
My rule is clarity first. Every rung must be easy to read for the next person. I always use consistent tag naming (e.g., “MOTOR_START” instead of “M1”) and structure programs into logical modules: start/stop sequences, safety interlocks, alarms, and production cycles. I also add comments for critical logic, so future technicians won’t waste time guessing.
I design from the operator’s point of view. That means clear HMI screens, logical button layouts, alarm messages written in plain language, and as few manual steps as possible. For example, instead of “Error Code 203,” the screen should say “Check left-side photoelectric sensor.” The machine should guide the operator, not confuse them.
Safety is built into the code as much as the hardware. I always add redundant checks for emergency stops, interlocks for guard doors, and fail-safes for critical motion. PLCs also make it possible to log safety events, which is important for CE and ISO compliance. My philosophy: a safe program is a reliable program.
I rely on standard modules for core functions—like motor start/stop, fault handling, and alarm logic. But every project needs customization, especially when clients use unique raw materials or production methods. The balance is to keep the backbone standardized, but allow flexible parameters for operators to adjust.
We use a mix of offline simulation and real machine dry runs. First, I simulate the sequence in the development software to check logical flow. Then, once the machine is assembled, I test each module separately—unwinder, slitter, rewinder—before running full production cycles. Only after stable runs at rated speed do I sign off the program.
I attend automation expos, study vendor updates (Siemens, Mitsubishi, etc.), and keep learning about Industry 4.0, IoT, and SCADA systems. At Jota, we’re exploring remote monitoring and predictive maintenance, so I also follow developments in sensor integration and cloud-based control.
Don’t just copy logic—understand why it works. Practice on small projects, learn both ladder logic and structured text, and get comfortable with electrical diagrams. Also, spend time on the workshop floor. Watching machines run teaches more than any classroom. And most importantly, always code as if someone else will debug your program tomorrow.
For me, it’s the moment the machine runs at full speed without alarms, and the customer smiles with relief. It’s like bringing something to life. My code may be invisible, but it drives every motion. That quiet satisfaction—knowing I turned lines of logic into real production—is why I love this work.